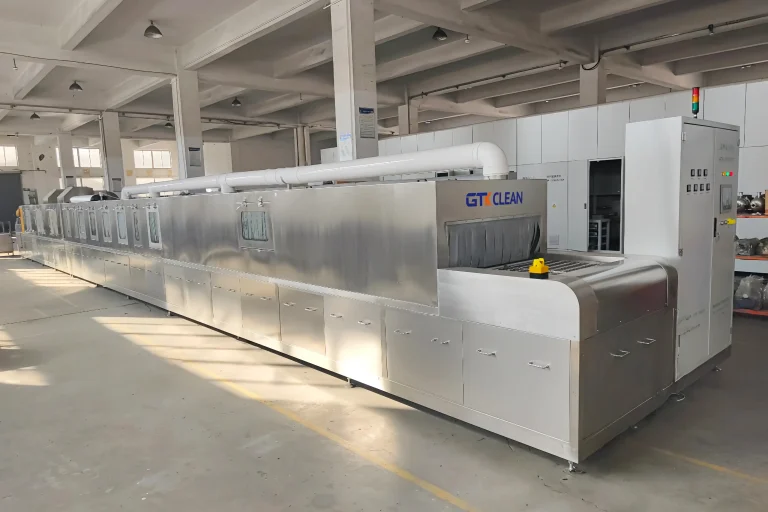
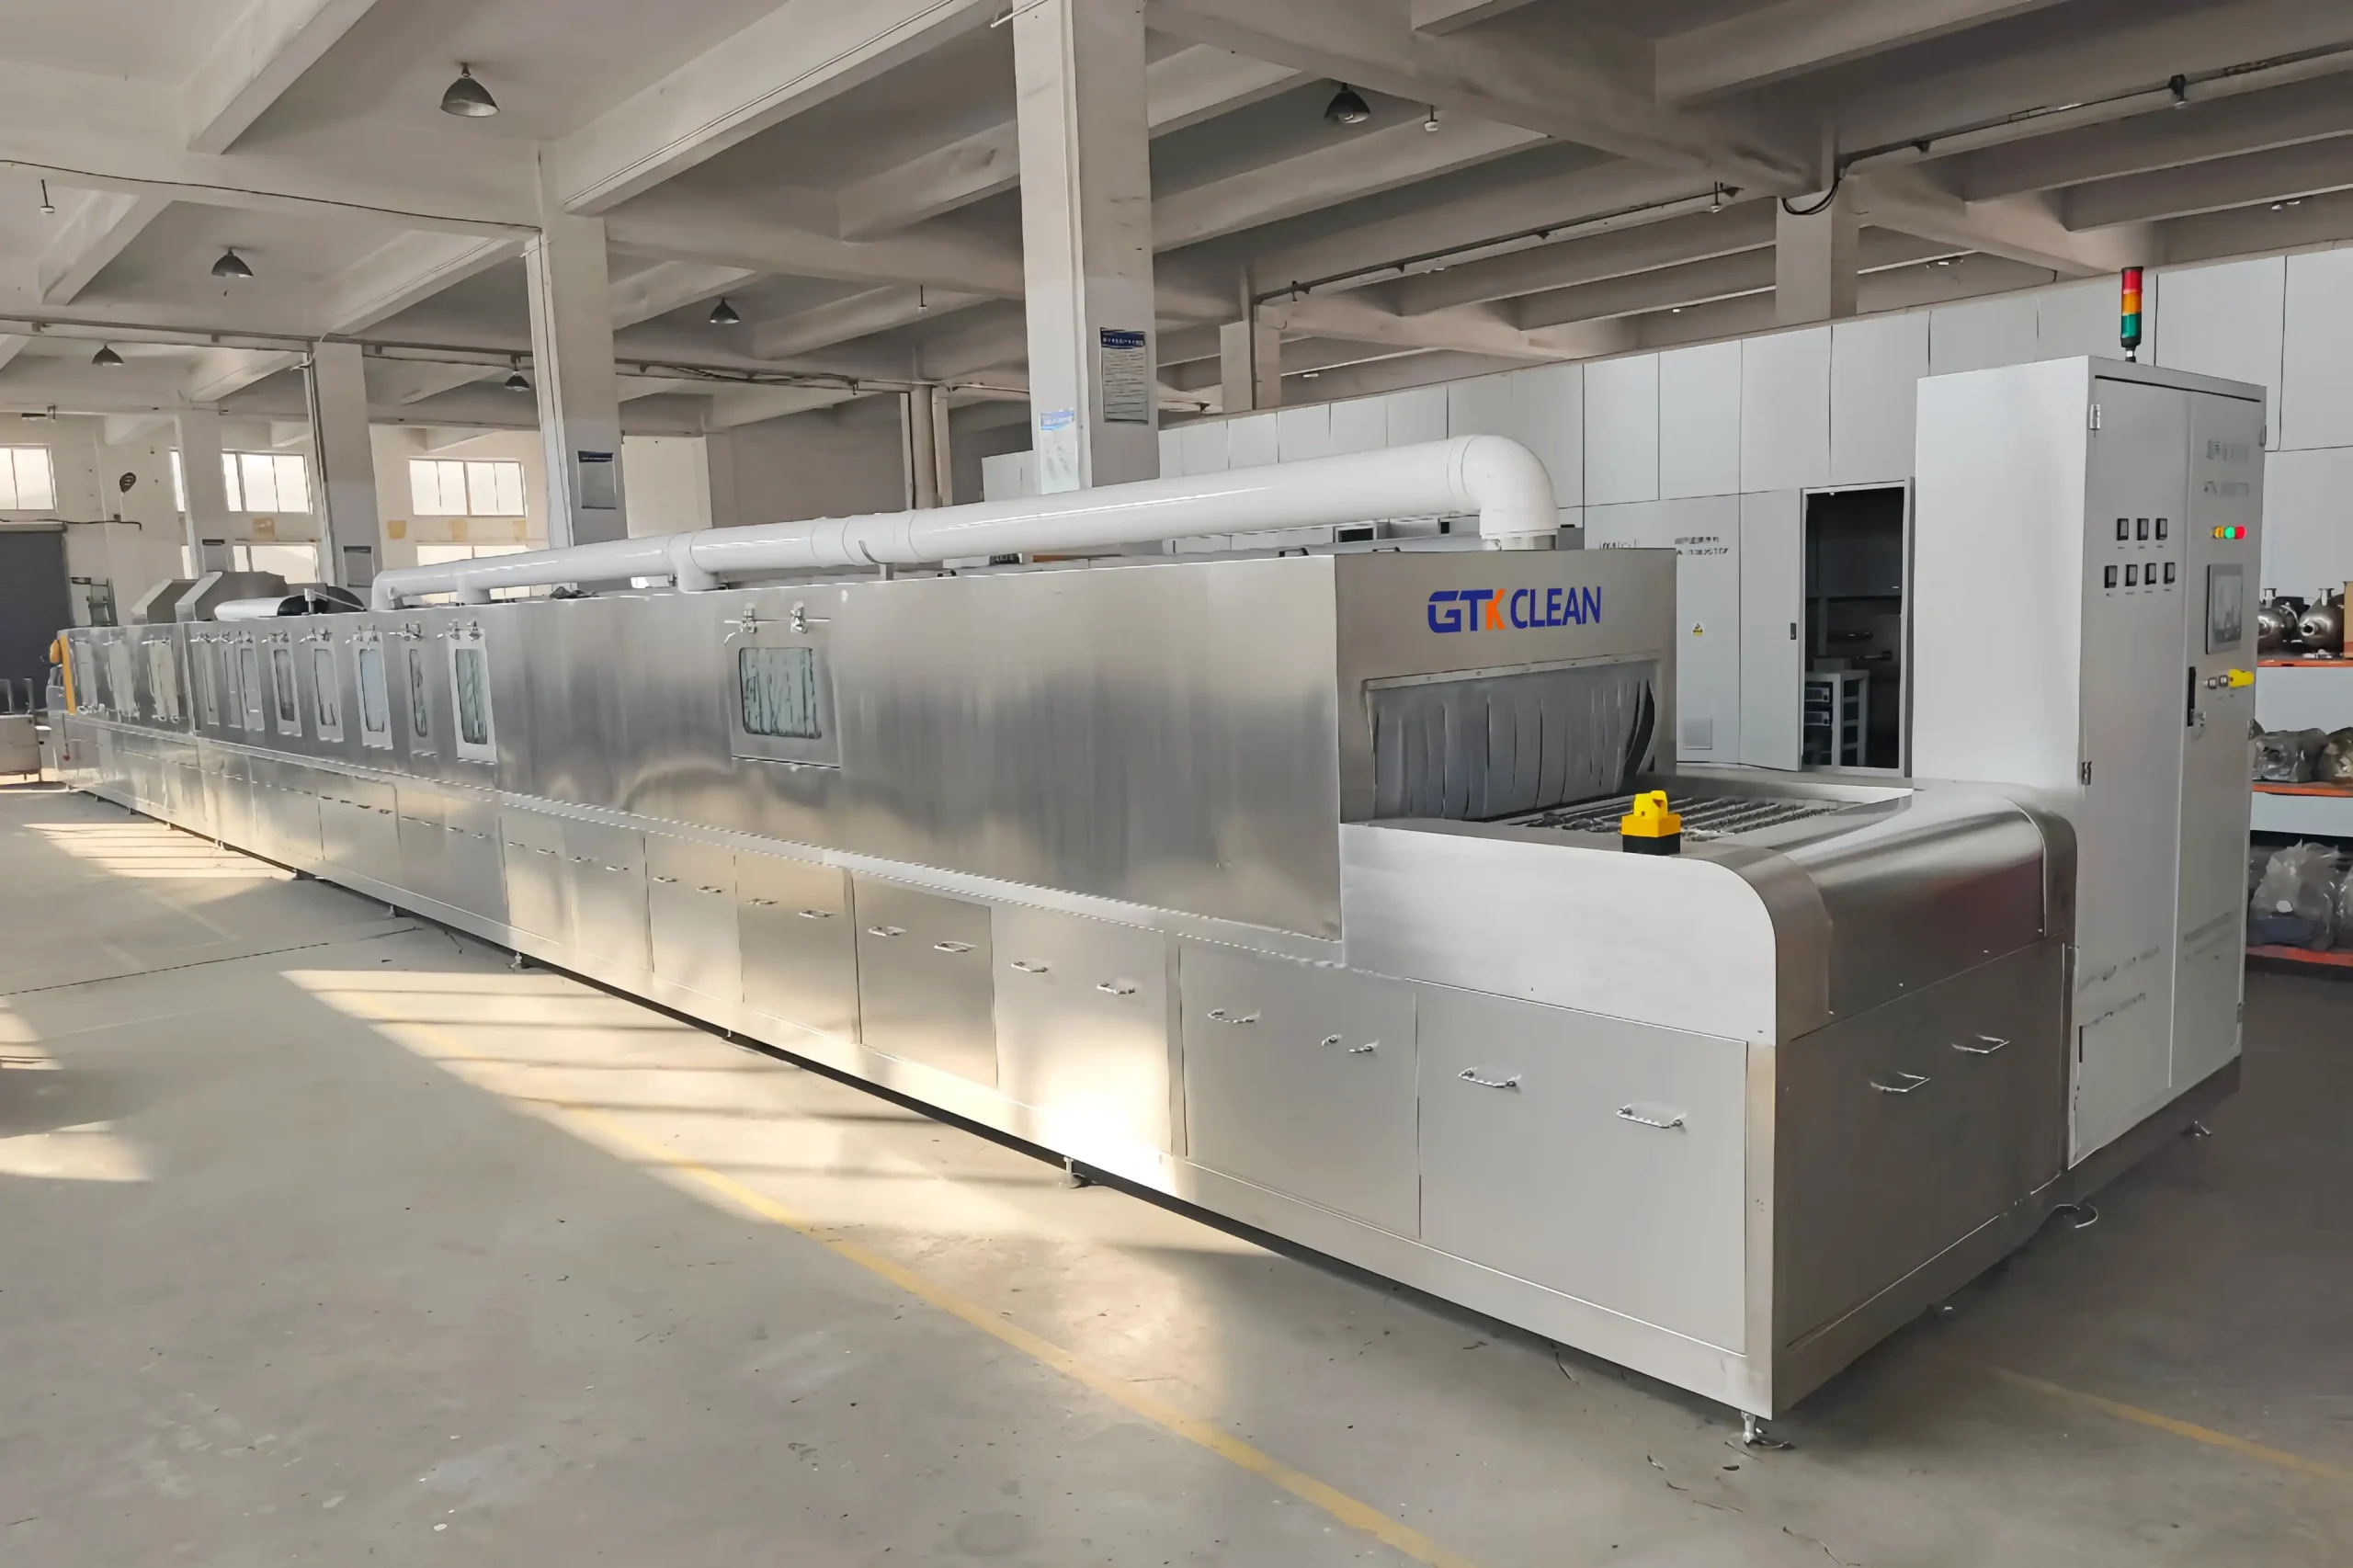
GTKClean engineers conveyor ultrasonic cleaners for manufacturers that need to combine continuous conveying with ultrasonic treatment for inline production flow.
Conveyor ultrasonic cleaners are designed to combine continuous conveying with ultrasonic treatment for inline production flow. Typical applications include small machined parts, stamped components, electronics and other repeatable high-throughput products.
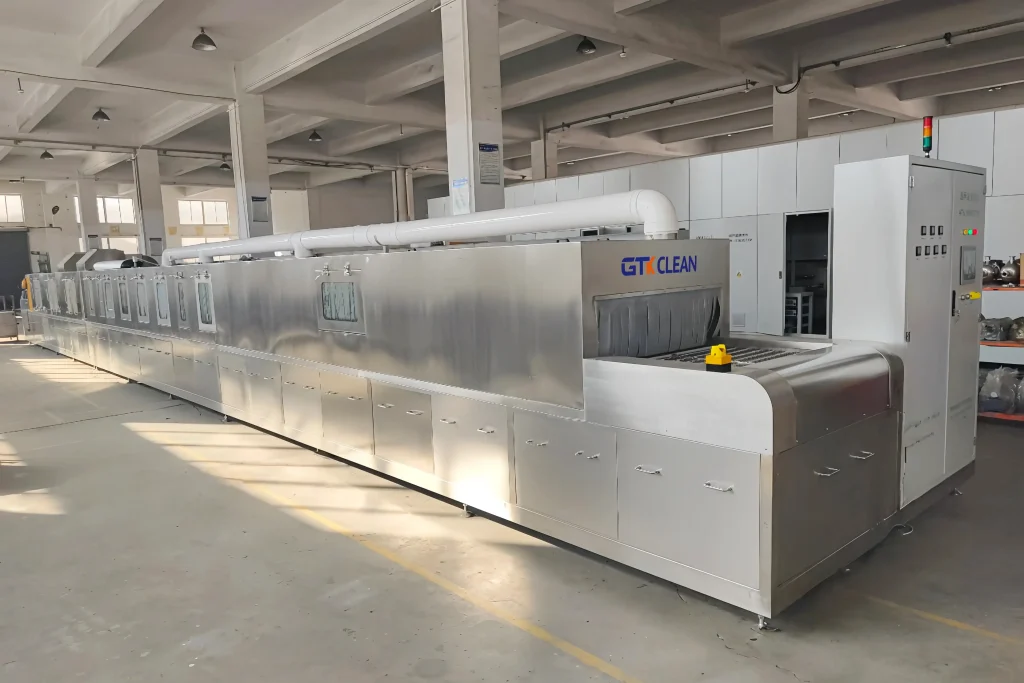
The process is configured from line speed, part retention, exposure time, conveyor material, carryover, rinsing and drying length. Available solutions can integrate mesh or fixture conveyors, ultrasonic zones, spray rinsing, air knives, filtration and line interlocks.
GTKClean uses application data and, where appropriate, representative sample parts to define the process before the final equipment configuration is approved.
Confirm part material and geometry, contaminant, cleanliness target, frequency, power density, chemistry, cycle time and automation level before the equipment or process is finalized.
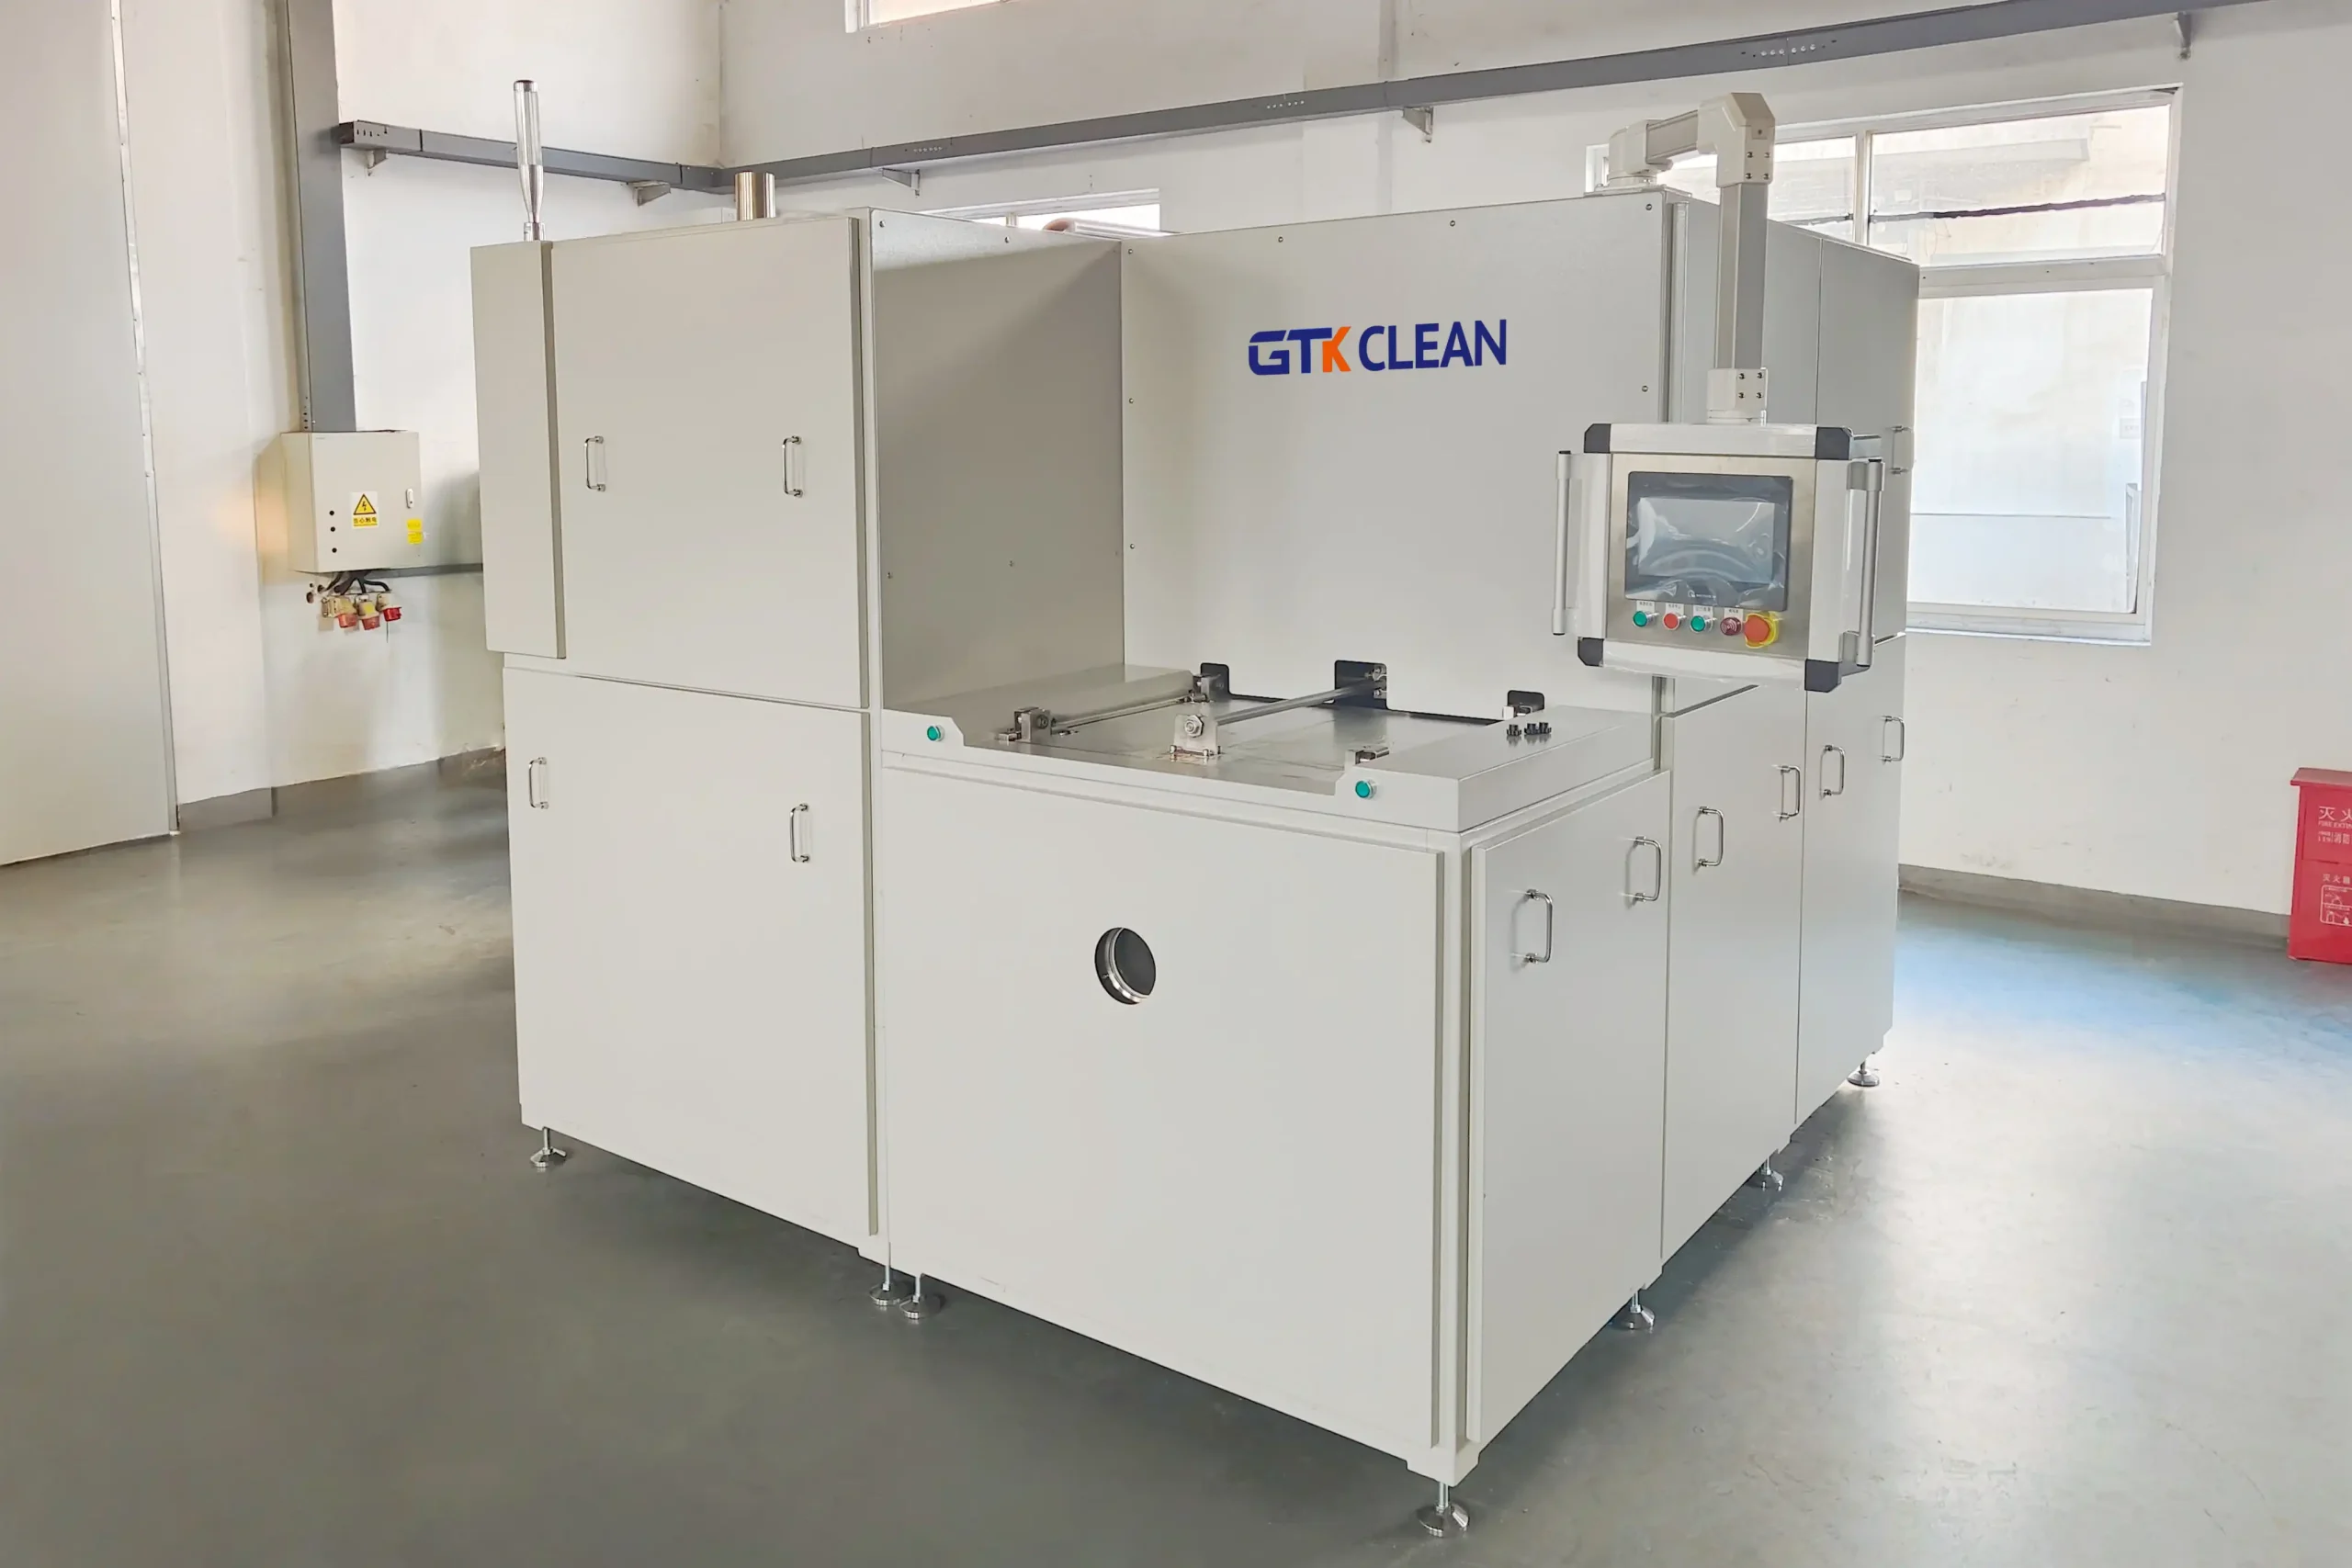
Use representative parts to define how the inline conveyor ultrasonic cleaning system will achieve the required result.
Develop the process layout, fluid circuit, controls, safety functions and operator access around the approved requirement.
Fabricate, assemble and inspect the stainless-steel structure, process modules, piping, wiring and handling system.
Run functional and process checks, document the approved configuration, then support installation, training and commissioning.
The process is defined around line speed, part retention, exposure time, conveyor material, carryover, rinsing and drying length, with sample testing available when results need verification.
The system can combine mesh or fixture conveyors, ultrasonic zones, spray rinsing, air knives, filtration and line interlocks according to the actual production requirement.
Mechanical, fluid, electrical and control functions are inspected against the approved project documents.
Documentation, commissioning guidance, training, spares and process review support stable long-term operation.
Conveyor Belt Ultrasonic Cleaners are a strong fit for small machined parts, stamped components, electronics and other repeatable high-throughput products.
The recommended layout depends on line speed, part retention, exposure time, conveyor material, carryover, rinsing and drying length. GTKClean compares process capability, throughput and maintainability before fixing the machine concept.
The equipment is engineered to combine continuous conveying with ultrasonic treatment for inline production flow.
A complete configuration can include mesh or fixture conveyors, ultrasonic zones, spray rinsing, air knives, filtration and line interlocks, with operating limits documented for the approved application.
Loading height, baskets, fixtures, recipes, traceability, safety circuits and communication interfaces can be adapted to the host production line.
Integration scope is agreed from drawings, signals, utilities, takt time and the responsibilities of each project party.
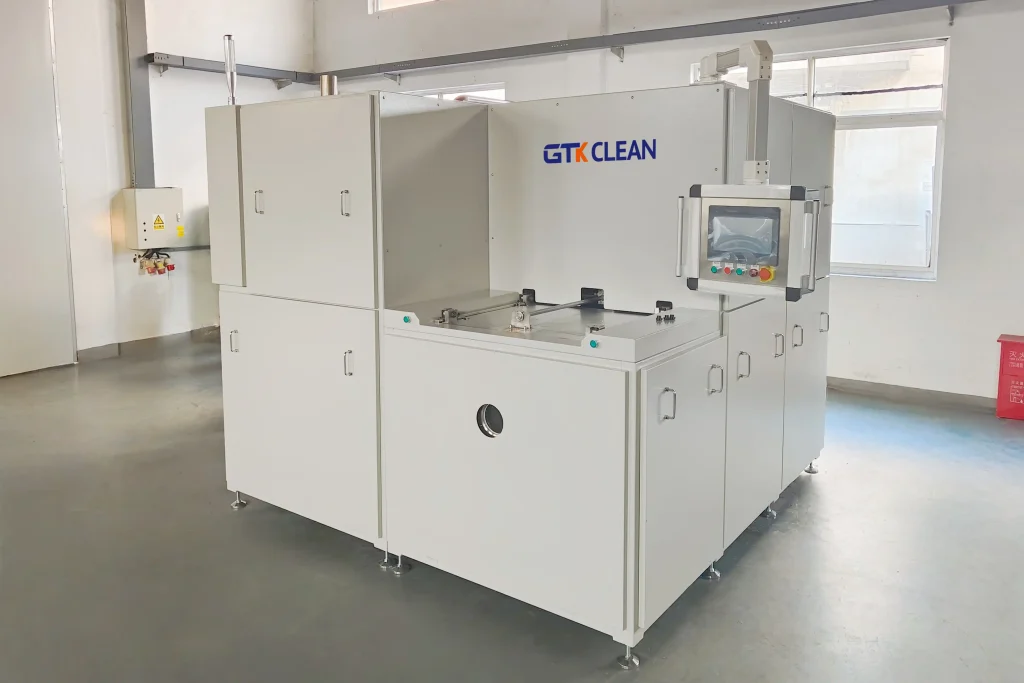
Inspection follows the approved drawings and technical proposal. Typical checks cover fabrication, installed components, piping, wiring, controls, alarms, safety functions and programmed operation.
For this category, acceptance planning should reflect line speed, part retention, exposure time, conveyor material, carryover, rinsing and drying length. When representative parts and a measurable standard are supplied, process trials can be documented before shipment.
The ultrasonic tank is sized from the required process capacity, operating conditions and interfaces for this product category.
The transducers and generator is sized from the required process capacity, operating conditions and interfaces for this product category.
The heating and circulation is sized from the required process capacity, operating conditions and interfaces for this product category.
The filtration and rinsing is sized from the required process capacity, operating conditions and interfaces for this product category.
The drying, handling and controls is sized from the required process capacity, operating conditions and interfaces for this product category.
Send part data, contamination, acceptance criteria and throughput so GTKClean can evaluate the appropriate process and equipment configuration.
Get a Project-Specific Quote
"Every Conveyor Belt Ultrasonic Cleaners project starts with the part, contamination and acceptance target. The equipment configuration follows the process requirement."
Conveyor ultrasonic cleaners are selected when manufacturers need to combine continuous conveying with ultrasonic treatment for inline production flow. The right solution is defined by the part, contamination and acceptance method—not by tank size or rated power alone.
GTKClean reviews sample parts, production data and factory constraints before proposing a process. This reduces the risk of buying equipment that looks suitable on paper but cannot meet the required cleanliness, throughput or operating cost.
The core process is designed to combine continuous conveying with ultrasonic treatment for inline production flow. Depending on the application, a complete cycle may combine mesh or fixture conveyors, ultrasonic zones, spray rinsing, air knives, filtration and line interlocks. Each stage has a defined operating window rather than relying on one fixed standard recipe.
Typical uses include small machined parts, stamped components, electronics and other repeatable high-throughput products. Suitability must still be confirmed against material compatibility, hidden geometry, soil loading and the way cleanliness will be measured after processing.
Important inputs include line speed, part retention, exposure time, conveyor material, carryover, rinsing and drying length. These values determine capacity, process sequence, utilities, controls and the level of automation required.
When the cleanliness target is critical, representative sample trials should reproduce the real contamination and inspection method. A visually clean part is not always sufficient for coating, assembly, optical or fluid-system service.
A project can incorporate mesh or fixture conveyors, ultrasonic zones, spray rinsing, air knives, filtration and line interlocks. GTKClean selects options only when they contribute to the required result, cycle time, bath stability, operator safety or integration with the production line.
Before delivery, checks can cover fabrication, piping, wiring, controls, alarms, safety interlocks, temperature, circulation and programmed sequences. When sample parts and an agreed test method are available, process results can be included in the factory acceptance plan.
Send this information through the GTKClean project enquiry form for an application-specific process and equipment proposal.