How to Prevent Flash Rust After Cleaning: A Practical Guide for Metal Parts
Table of Contents
- Why Flash Rust Forms After Cleaning
- Six Variables That Decide Whether Parts Rust
- Start With Water Chemistry and Rinse Water Quality
- Move Parts Into Drying Quickly
- Use Rust Inhibitors Only Where They Help
- Build the Right Equipment Sequence
- Frequently Asked Questions
- Why does flash rust appear so quickly on freshly cleaned steel?
- Can hot water help prevent flash rust?
- Does rust inhibitor have to be removed before coating?
- Is flash rust mainly an aqueous cleaning problem?
- How do I check for flash rust without slowing production?
- What is the fastest line-side fix for flash rust?
- References
Flash rust is the thin oxide film that can form on bare steel or iron surfaces within minutes after aqueous cleaning. It is often light enough to wipe away, but if it stays under a coating, adhesive, or assembly lubricant, it becomes a hidden bond breaker. Flash rust is best understood as a process outcome, not a material defect. By controlling water chemistry, minimizing wet dwell time, moving parts quickly into drying, and selecting the right temporary inhibitor, most production teams can prevent repeated failures without changing the entire cleaning technology.
Why Flash Rust Forms After Cleaning
During aqueous cleaning, detergent films, cutting fluids, and light oxides are removed from the metal surface. The exposed steel is highly active. When oxygen, water, and the iron surface meet, a thin oxide layer forms. The reaction accelerates when dissolved salts increase conductivity, when the pH moves outside a near-neutral range, or when the part remains wet and warm. Residual cleaner trapped in threads, blind holes, or stacked parts can also hold moisture long after the visible surface looks dry.
Inspectors often compare the extent of the bloom against visual rust-grading standards such as ISO 8501-1 [1] to decide whether the surface can proceed to the next operation. That comparison matters because light discoloration and heavy bloom require different responses.
Aqueous cleaning creates the widest flash-rust window because the part leaves the rinse stage wet and alkaline residues can remain in recesses. <How to Choose Between Aqueous and Solvent Cleaning Systems> covers when a solvent or vacuum-drying approach can shorten the wet window and reduce oxidation risk.
Six Variables That Decide Whether Parts Rust
Flash rust prevention is a balance of several interacting variables:
- Base metal and surface condition
- Previous process residues
- Rinse water quality and conductivity
- Final rinse temperature
- Drainage and transfer dwell time
- Drying method and airflow access
Changing only one variable often moves the problem rather than removing it. A faster dryer does not help if parts are loaded so tightly that air cannot reach internal surfaces. A clean rinse does not help if wet baskets wait beside the line before drying.
Start With Water Chemistry and Rinse Water Quality
Municipal water can contain chlorides, hardness minerals, and other dissolved solids that leave a conductive film on the part surface. For final rinses, deionized water or reverse-osmosis water is often used when the final cleanliness requirement is high. The purpose is not only residue removal. Lower conductivity reduces the electrolyte available for the oxidation reaction.
Final rinse temperature should also be managed. Warm rinse water can help drying, but if the part remains wet at an elevated temperature, oxidation can occur more quickly. The process should use warm rinse temperatures only when transfer to drying is immediate.
Move Parts Into Drying Quickly
After the final rinse, wet dwell time is one of the most controllable variables. Blow-off stations, air knives, hot air, or vacuum drying can remove surface water and water trapped in blind holes or recesses. The most effective drying method depends on part geometry: flat parts may dry quickly with forced air, while complex parts often need vacuum drying or multiple air-knife angles.
Basket orientation and load density also matter. If parts nest or cup water, rust will appear even when the outer surfaces are dry.
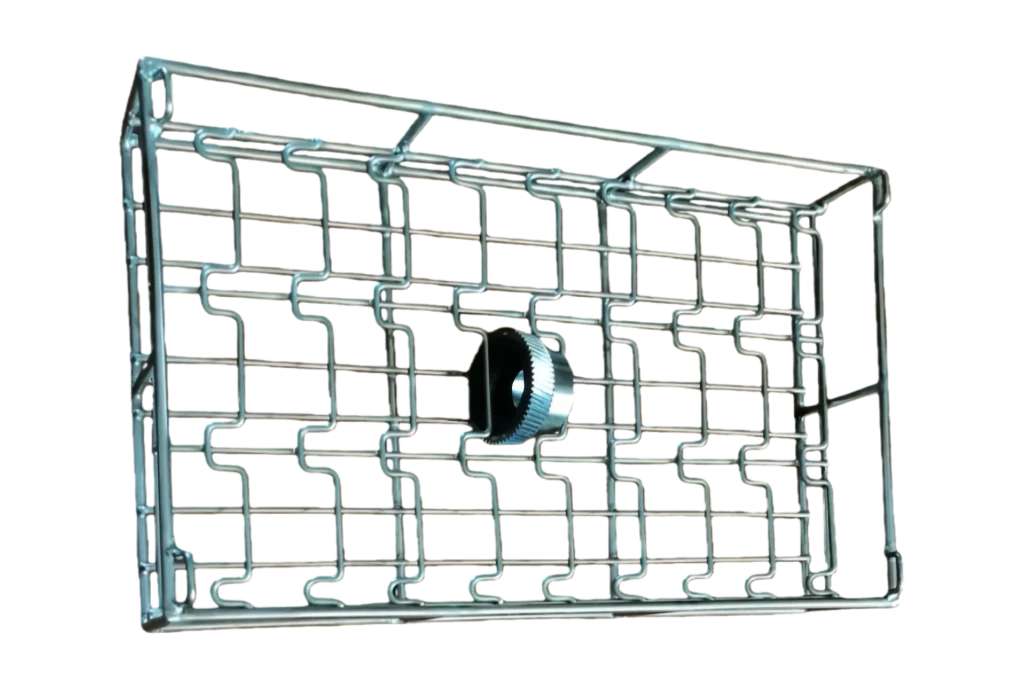
Dwell time between rinse and drying matters more than many teams realize. <Inline Ultrasonic Washing Systems for Enhanced Process Control> covers how automated transfer and step timing keep the wet interval short and repeatable.
Use Rust Inhibitors Only Where They Help
A water-soluble rust inhibitor in the final rinse is a practical safeguard when parts cannot be dried immediately. The inhibitor leaves a temporary protective film that reduces oxidation during short-term storage or transfer. Compatibility with the next operation is the deciding factor. A film that protects bare steel may interfere with paint adhesion, welding, adhesive bonding, or subsequent plating.
For stainless steel that shows rust staining after cleaning, the cause is often iron contamination from tooling or shared baskets rather than oxidation of the stainless itself. In those cases, passivation according to a standard such as ASTM A967 [2] may be more effective than adding a general rust inhibitor.
If the parts are headed to coating, cleaning and final surface condition need to be treated as one chain. <Ultrasonic Pre-Cleaning Machine for Flawless PVD/DLC Coating Pre-Treatment> covers how pre-cleaning, rinsing, and drying are combined to prevent surface defects before coating.
Build the Right Equipment Sequence
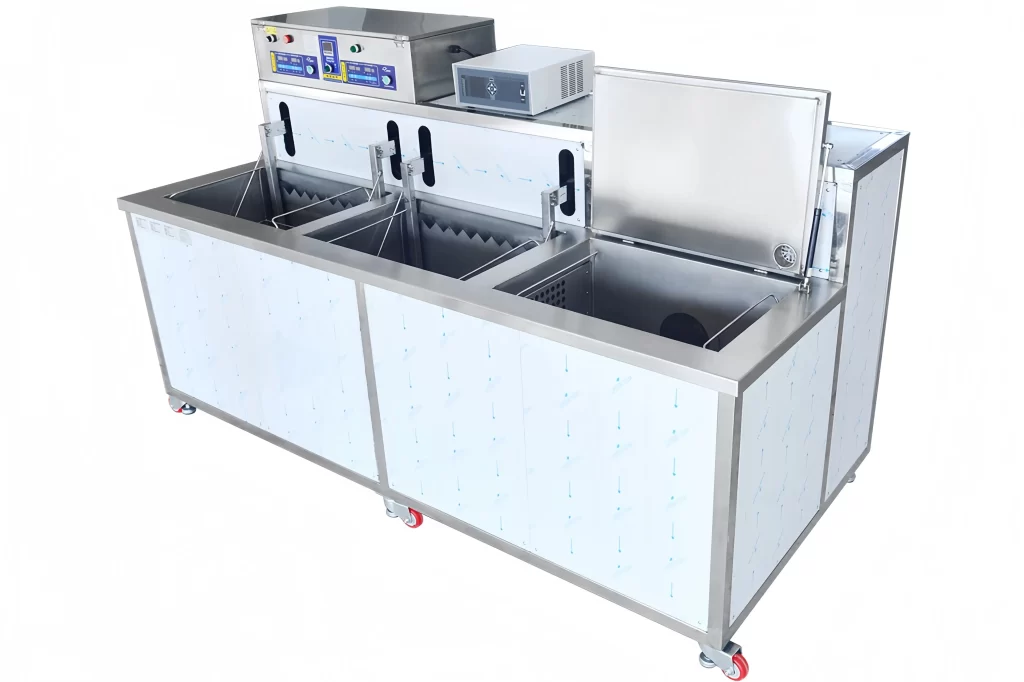
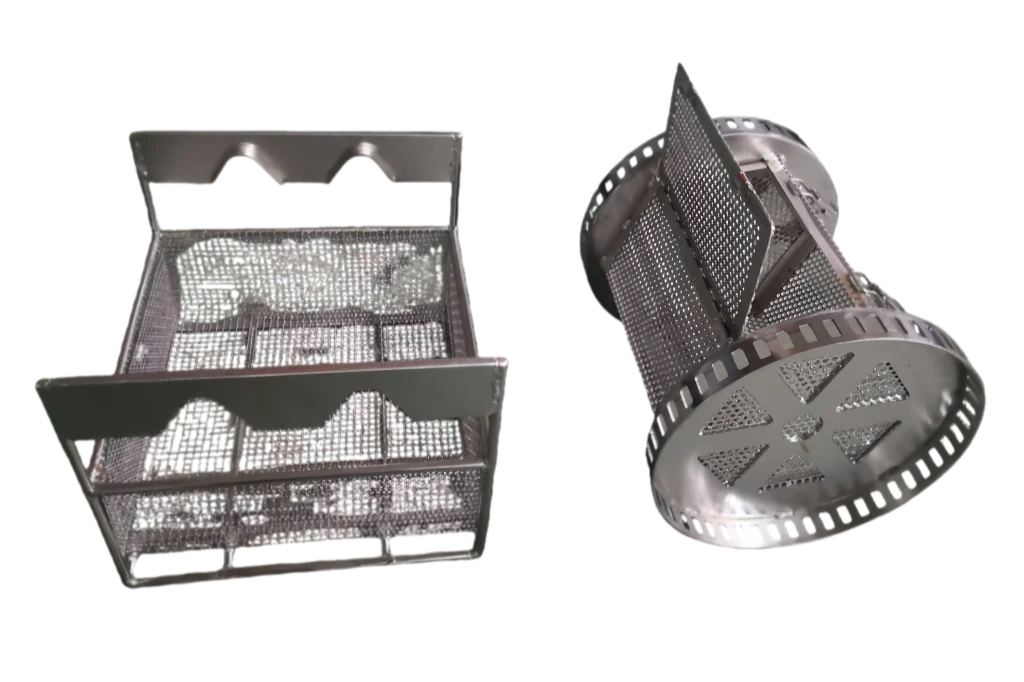
Multi-tank systems with separated wash, rinse, and drying zones reduce the carryover that prolongs wet time. Automated transfer removes the variability of manual basket handling and keeps the interval between rinse and dry consistent. Basket design should allow water to drain freely, and load size should not exceed what the dryer can realistically remove.
For high-volume production, a multi-tank line with final DI rinse and controlled drying is often the most repeatable way to prevent flash rust. The equipment sequence, not a single stronger chemical, provides the real process control.
Get a flash-rust control recommendation. If you are seeing recurring rust on cleaned steel, send GTKCLEAN a description of the part material, maximum dimensions and weight, current cleaning sequence, rinse water, dryer type, and whether parts are coated, welded, or assembled afterward. Contact Li Hao at [email protected] or +86 17768507147 for a process review before purchasing new equipment.
Frequently Asked Questions
Why does flash rust appear so quickly on freshly cleaned steel?
Freshly cleaned steel is highly active. Once detergent films and light oxides are removed, oxygen and water can react with the exposed metal surface very quickly, especially when heat, salts, or trapped moisture are present.
Can hot water help prevent flash rust?
Hot water can speed drying, but it can also accelerate oxidation while the part is still wet. Warm rinse water works well only when transfer to drying is short. Otherwise, hot water may increase the risk of flash rust.
Does rust inhibitor have to be removed before coating?
It depends on the inhibitor and the coating. Some temporary inhibitors can reduce paint, adhesive, or plating adhesion. Compatibility with the downstream process should be confirmed before using an inhibitor in the final rinse.
Is flash rust mainly an aqueous cleaning problem?
Aqueous cleaning creates the most common flash-rust window because the part remains wet after rinsing. Solvent systems reduce free water, but rust can still form if moisture enters the solvent or if parts condense after cleaning.
How do I check for flash rust without slowing production?
Inspect parts immediately after drying in good light. Compare the surface against a visual standard such as ISO 8501-1 [1] and record whether the discoloration is light, moderate, or heavy. Early detection helps identify the process variable before parts reach coating or assembly.
What is the fastest line-side fix for flash rust?
Shorten the dwell time between rinse and drying, improve blow-off coverage, reduce load density, and check whether baskets are trapping water. If the problem continues, add a compatible rust inhibitor to the final rinse while investigating water quality.
References
[1] ISO 8501-1:2007, Preparation of steel substrates before application of paints and related products — Visual assessment of surface cleanliness — Part 1: Rust grades and preparation grades of uncoated steel substrates.
[2] ASTM A967/A967M-17, Standard Specification for Chemical Passivation Treatments for Stainless Steel Parts.
If you’re interested, check out these related articles:
Automated Ultrasonic Cleaning: Elevating Industrial Process Consistency
Optimizing Industrial Cleaning to Reduce Solution Expenses
Automotive Parts Cleaning Solutions – GTK
Boost Automotive Manufacturing Cleaning Efficiency: A Strategic Guide
Industrial Ultrasonic Cleaning Systems: The Complete Guide