Passivation and Metal Preparation Explained: Process Guide
Table of Contents
- What Metal Preparation Includes Before Passivation
- What Passivation Actually Does
- Passivation vs Pickling vs Cleaning
- Nitric Acid vs Citric Acid Passivation
- Passivation Process and Critical Control Points
- Common Passivation Failures and Preventive Measures
- How Cleaning Equipment Supports Repeatable Passivation
- Engineering Support for Passivation and Metal Preparation
- FAQ
- Is passivation the same as pickling?
- Can carbon steel be passivated?
- Does passivation remove machining oil?
- What final rinse water quality is needed?
- How is passivation verified?
- References
Passivation is often treated as a standalone chemical bath, but in a production line it only works after the right metal preparation sequence. Without effective cleaning, free iron, heat tint, machining residues, and rinse contamination stay on the surface and interfere with the formation of a passive oxide layer. This article explains how passivation works, where it fits in metal preparation, and which process controls determine whether parts leave the line protected and coating-ready.
What Metal Preparation Includes Before Passivation
Metal preparation is the complete sequence that makes a component chemically and physically ready for the next operation. For stainless steel and other corrosion-resistant alloys, preparation usually includes:
- Removal of machining oils, cutting fluids, chips, and shop dust
- Removal of oxide scale, weld tint, and heat-treatment discoloration
- Removal of iron contamination smeared onto the surface by tools, fixtures, or handling
- Rinsing to remove cleaning chemistry and dissolved contamination
- Final drying that prevents water spots and flash rust
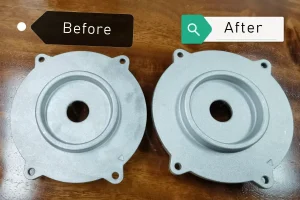
Cleaning and passivation are not interchangeable. Cleaning removes external soil; passivation removes or neutralizes surface iron and establishes a corrosion-resistant chromium oxide film. If cleaning is incomplete, the acid bath must work through oil films and heavy soil before it can reach the base metal, which produces uneven results.
Effective preparation usually uses staged equipment such as spray prewash, ultrasonic cleaning, rinse tanks, and drying modules. Multi-tank systems are common because they separate each chemistry and prevent cross-contamination between cleaning, rinsing, and passivation.
What Passivation Actually Does
Passivation improves the natural corrosion resistance of stainless steel. Stainless alloys resist corrosion because chromium in the metal reacts with oxygen to form a thin, adherent, chromium-rich oxide layer. However, manufacturing operations can leave free iron on the surface. That free iron corrodes quickly and creates initiation points for pitting, staining, or coating failure.
The passivation bath dissolves surface iron and other tramp contaminants while allowing the chromium oxide film to form uniformly. The acid does not remove heavy scale or weld tint; that is the role of pickling. Passivation is a relatively mild chemical treatment intended for clean parts that still carry invisible surface iron and process residues [1].
This distinction matters for metal preparation. A part with weld scale or heat tint should be pickled or mechanically descaled first. A part that is already dimensionally finished and clean can go directly to passivation.
Passivation vs Pickling vs Cleaning
The table below separates three processes that are frequently confused in surface preparation.
| Process | Main target | Chemical action | Surface result |
|---|---|---|---|
| Cleaning | Chips, oil, grease, particulate, light residues | Detergents, solvents, spray, ultrasonic action | Visible surface free of gross soil |
| Pickling | Weld tint, heat scale, heavy oxides | Strong acid, often nitric plus hydrofluoric acid | Scale removed; surface lightly etched |
| Passivation | Free iron, trace contamination, passive film formation | Nitric or citric acid treatment | Corrosion-resistant chromium oxide layer |
Passivation is normally not a substitute for pickling. Sending scaled parts directly into a passivation bath can leave scale behind and consume acid without forming a uniform passive layer [1][3].
Nitric Acid vs Citric Acid Passivation
ASTM A967 recognizes both nitric acid and citric acid methods for passivating stainless steel [1]. Aerospace and industrial specifications such as AMS 2700 also govern many applications [2].
| Variable | Nitric acid method [1][2] | Citric acid method [1][2] |
|---|---|---|
| Typical chemistry | 20–50% nitric acid by volume | 4–10% citric acid by weight |
| Temperature range | Ambient to about 60°C | Often 60–70°C |
| Immersion time | Typically 20–60 minutes | Typically 10–30 minutes |
| Main strength | Strong oxidizing action, long industry history | Safer handling, chelation of iron, easier waste treatment |
| Watch points | Fumes, acid handling, NOx generation | Bath loading, temperature control, iron saturation |
Citric acid has become more common for precision parts because it is safer to handle and less aggressive to dimensional tolerances. The correct choice depends on alloy, final application, customer specification, and production-safety review. Do not change from nitric to citric acid simply to match a bath temperature; the entire process must be validated against the applicable standard [1][2].
Passivation Process and Critical Control Points
A typical passivation sequence is:
- Alkaline or detergent precleaning
- Initial rinse
- Acid passivation bath
- Cascade or overflow rinse
- Deionized-water final rinse
- Drying
| Stage | Purpose | Key control |
|---|---|---|
| Preclean | Remove oils, chips, drawing compound, particulate | Time, temperature, detergent concentration, mechanical action |
| Initial rinse | Remove cleaning chemistry | Flow rate, pH, water quality |
| Passivation bath | Dissolve free iron, promote passive oxide | Acid concentration, temperature, immersion time, agitation |
| Cascade rinse | Dilute and remove acid | Overflow rate, number of stages |
| Final DI rinse | Prevent mineral deposits and chloride residues | Conductivity or resistivity, pH, rinse time |
| Drying | Prevent flash rust and water spots | Part temperature, air cleanliness, drainage |
Water quality is one of the most underrated variables. A final rinse with hard water or chloride-containing water can leave spots and corrosion cells on a passivated surface. ASTM A380 addresses cleaning and passivation of stainless steel parts and systems, including the importance of clean, low-chloride rinse water [3]. In precision applications, the final rinse should be dbuy deionized water with controlled conductivity and adequate overflow.
Passivation verification is part of the process, not an afterthought. ASTM A967 lists tests such as water immersion, high-humidity exposure, salt spray, copper sulfate, and ferroxyl testing [1]. The appropriate test depends on the part risk level, material grade, and customer requirement.
Common Passivation Failures and Preventive Measures
Most passivation problems are not caused by the acid bath alone. They trace back to preparation, rinsing, or handling.
| Failure | Typical cause | Preventive action |
|---|---|---|
| Flash rust after passivation | Poor rinsing, contaminated final rinse, wet storage | Use clean DI rinse, dry immediately, protect parts from humid air |
| Etching or pitting | Excess acid concentration, high temperature, long immersion | Control bath parameters, verify grade and part condition |
| Water spots | Hard water or mineral-laden final rinse | Use deionized water, overflow rinsing, controlled drying |
| Uneven passivation | Oil or residue on part, trapped air in blind holes | Improve precleaning, use agitation or fixturing |
| Copper sulfate test failure | Free iron not fully removed | Check bath life, temperature, time, and surface cleanliness |
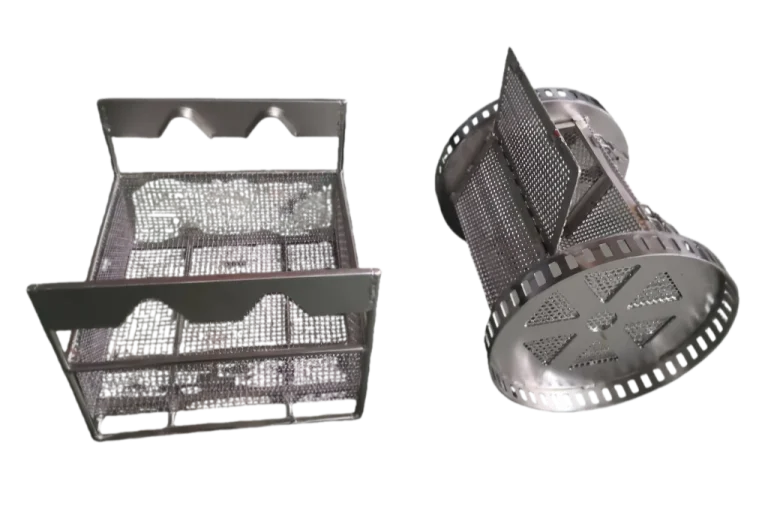
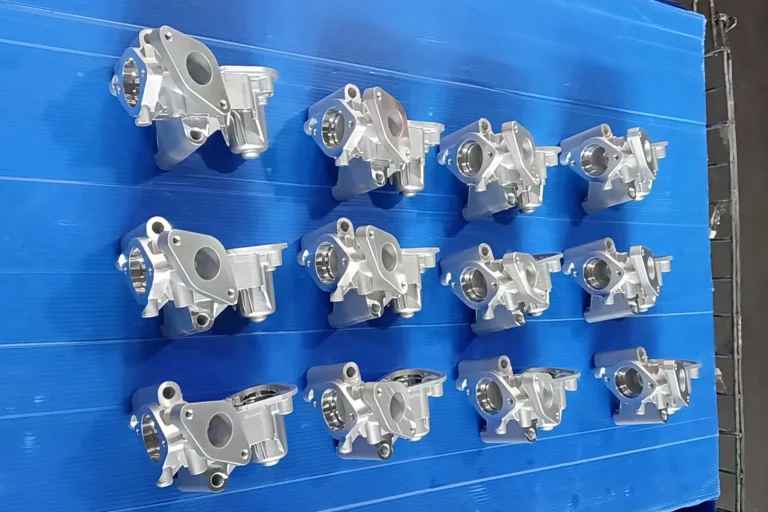
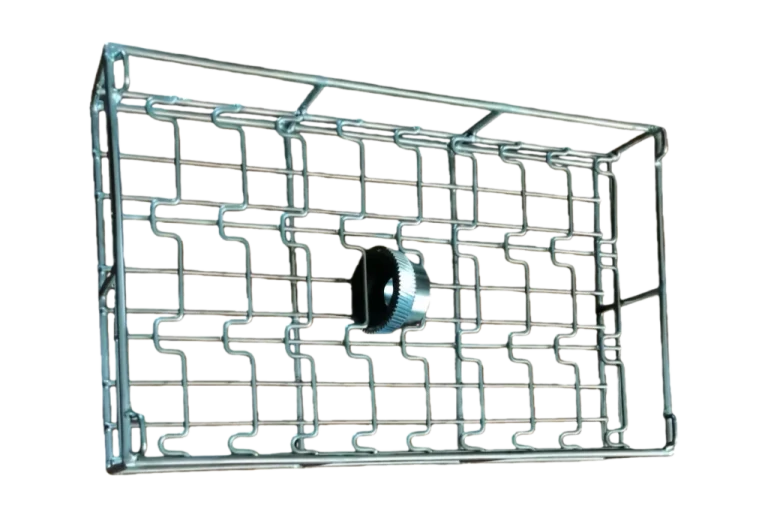
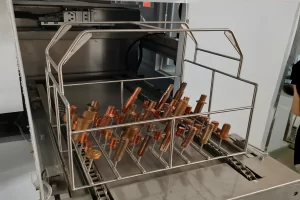
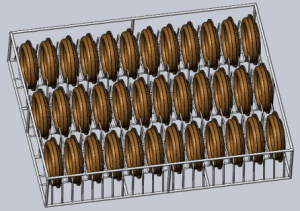
Blind holes, threads, and narrow gaps require particular attention. These features trap cleaning chemistry, acid, or rinse water, and they can carry contamination into the passivation bath. Basket design and part orientation should promote drainage at every stage. A washing basket that holds parts too tightly or blocks internal features can create isolated areas that never see proper flow.
Residue left on the surface before coating creates the same failure chain as passivation residue. <Eliminate Residue in Pre-Coating Parts Cleaning: An Expert Guide> covers how to control final-stage contamination and verify cleaned surfaces.
How Cleaning Equipment Supports Repeatable Passivation
Passivation is highly sensitive to surface consistency. Manual cleaning may be acceptable for low-volume or simple parts, but production lines with mixed part numbers benefit from automated multi-stage equipment. Automation controls soak time, rinse time, temperature, and transfer, reducing the variation that causes lot-to-lot passivation failures.
A pre-coating ultrasonic cleaning line, for example, may combine spray prewash, ultrasonic degreasing, multi-stage ultrapure water rinsing, and hot-air or vacuum drying. In one GTKCLEAN pre-PVD system design, the ultrapure water system targets conductivity of 0.06 µS/cm or less to prevent water spots and secondary contamination before coating. That same control logic applies to passivation lines: the cleaner the surface before chemical treatment, the more uniform the passive film.
Pre-treatment cleaning determines how well PVD or DLC coatings bond to the substrate. <Ultrasonic Pre-Cleaning Machine for Flawless PVD/DLC Coating Pre-Treatment> covers multi-stage ultrasonic cleaning and ultrapure water rinsing before coating.
Passivation and precision cleaning both depend on the same surface-preparation fundamentals. <Pre-Coating Cleaning Solutions for PVD – GTK> covers process sequences for coating-ready metal surfaces.
If you are specifying a passivation stage or updating a manual wash line, send your substrate, part geometry, contaminants, and required cleanliness standard to [email protected]. Engineering can review the sequence and recommend where ultrasonic cleaning, DI-water rinsing, and passivation should sit in the line.
Engineering Support for Passivation and Metal Preparation
A reliable passivation process starts with a cleaning line that delivers the same surface condition batch after batch. For an engineering review, contact GTKCLEAN with the following information:
- Part material and grade, such as 304, 316L, or 17-4 PH
- Contamination present before cleaning: oil, chips, scale, rust, fingerprints, or polishing compound
- Part geometry, including blind holes, threads, and internal cavities
- Required throughput, basket load, and part weight
- Next process after cleaning: coating, welding, assembly, or storage
- Cleanliness or passivation specification to meet
Email [email protected] or call +86 17768507147 to request a process sequence or line configuration review. The goal is not only to select a passivation chemistry, but to engineer the full preparation chain so the passive layer forms consistently on every part.
FAQ
Is passivation the same as pickling?
No. Passivation removes free iron and promotes a passive chromium oxide film on stainless steel. Pickling removes heat tint, weld scale, and heavy oxides using stronger acid and may lightly etch the surface.
Can carbon steel be passivated?
Carbon steel does not form the same self-protecting chromium oxide film as stainless steel. It can be cleaned and protected with rust preventives or coatings, but the process should not be described as passivation in the stainless-steel sense.
Does passivation remove machining oil?
No. Passivation is not a degreasing step. Parts must be cleaned before passivation. Leaving oil or cutting fluid on the surface can produce uneven treatment and contaminate the bath.
What final rinse water quality is needed?
The final rinse should use clean, low-chloride water, preferably deionized water with controlled conductivity. Hard water or chloride-bearing tap water can leave mineral residues and corrosion cells on passivated parts.
How is passivation verified?
ASTM A967 lists several verification tests, including water immersion, high-humidity exposure, salt spray, copper sulfate, and ferroxyl testing. The selected method depends on material grade, part risk, and customer requirements.
References
[1] ASTM International, A967/A967M, Standard Specification for Chemical Passivation Treatments for Stainless Steel Parts, ASTM International, West Conshohocken, PA.
[2] SAE International, AMS 2700, Passivation of Corrosion Resistant Steels, SAE International, Warrendale, PA.
[3] ASTM International, A380/A380M, Standard Practice for Cleaning, Descaling, and Passivation of Stainless Steel Parts, Equipment, and Systems, ASTM International, West Conshohocken, PA.
If you’re interested, check out these related articles:
Leasing Versus Buying Industrial Cleaning Equipment Strategic Guide
Multi-Tank Ultrasonic Cleaning: A Deep Dive into Industrial Configurations
Industrial Ultrasonic Cleaning Systems: The Complete Guide
How to Select the Frequency for Ultrasonic Cleaning Equipment ?
Choosing the Right Ultrasonic Cleaning System for Your Factory